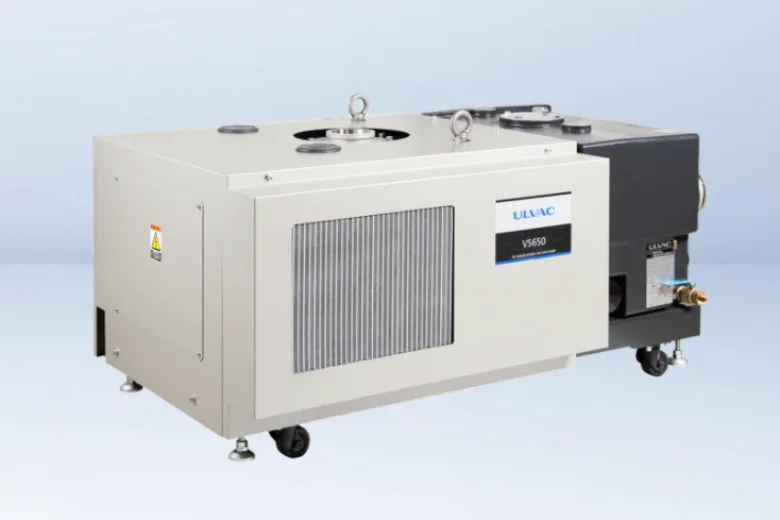
ULVAC VS Series Large-Capacity Oil-Sealed Rotary Vane Vacuum Pump
The ULVAC VS Series is a single-stage oil-sealed rotary vane vacuum pump developed for industrial vacuum applications requiring high pumping capacity. Thanks to its robust mechanical construction, high pumping speed, and design suitable for continuous operation, it delivers reliable vacuum performance under heavy-duty operating conditions. Its built-in oil mist separator, automatic oil return system, and large-capacity oil reservoir ensure stable long-term operation while extending maintenance intervals.
Key Features
- High-capacity single-stage rotary vane design
- Available in both air-cooled and water-cooled models
- Designed for direct installation of a mechanical booster pump
- Built-in oil mist separator and automatic oil return system
- Large-capacity oil reservoir for extended oil change intervals
- Easy maintenance with a cartridge-type oil mist filter
- Built-in oil filter for clean oil circulation and extended equipment life
- Standard thermostat for monitoring pump temperature and oil level
- Robust mechanical construction designed for continuous industrial operation
Application Areas
VS Series vacuum pumps are widely used in industrial vacuum applications requiring high pumping capacity:
- Optical film coating systems
- Thin film deposition systems
- Decorative vacuum coating systems
- Roll-to-roll coating systems
- In-line sputtering systems
- Vacuum heat treatment furnaces
- Vacuum freeze drying systems
- Helium leak testing systems
- Space simulation chambers
- Large-scale industrial vacuum systems
Technical Advantages
The VS Series offers solutions for high-capacity vacuum applications with the VS650B and VS750B models. With pumping capacities ranging from approximately 650 m³/h to 750 m³/h, the series delivers outstanding performance in high-throughput processes with an ultimate pressure of up to 8 Pa (0.08 mbar). Thanks to its compatibility with mechanical booster pumps, availability in both air-cooled and water-cooled configurations, built-in oil mist separator, and automatic oil return system, it provides long-term, reliable, and low-maintenance operation, making it an ideal vacuum solution for heavy industry and advanced technology manufacturing facilities.